
How Are Batteries Manufactured?
As the core power carrier in the new energy era, the production process of lithium batteries integrates the top achievements of materials science, precision manufacturing and intelligent technology. From the perspective of the entire industry chain, this article deeply analyzes the complete production process of lithium batteries from "powder" to "battery cell", covering key links such as material preparation, electrode coating, battery cell assembly, and formation testing, and combines process parameters and equipment selection to help you master the underlying logic of lithium battery manufacturing.
1. Raw material processing
70% of the performance of lithium batteries is determined by raw materials. The ratio and pretreatment of positive and negative active materials, conductive agents, and binders are the starting point of the manufacturing process.
1.1 Preparation of positive electrode materials
- Raw material mixing: lithium cobalt oxide (LCO), lithium iron phosphate (LFP) or ternary material (NCM) is used as the matrix, and mixed with conductive agents (such as superconducting carbon black) and binders (PVDF) in proportion.
- Preparation of glue solution: When using the wet process, PVDF needs to be dissolved in N-methylpyrrolidone (NMP) to form a glue solution with stable viscosity (viscosity range 2000-4000mPa·s).
- Slurry dispersion: High-speed dispersion is performed by a planetary mixer under vacuum (≤-0.085MPa) to ensure uniform distribution of active substances (particle size ≤15μm).
1.2 Preparation of negative electrode materials
- Graphite pretreatment: Natural/artificial graphite is mixed with conductive agent (carbon nanotubes) and binder (SBR, CMC) after ball milling and screening, and an aqueous solvent (deionized water conductivity ≤1μs/cm) is used.
- Slurry stability control: Long-chain molecular breakage is avoided by staged mixing (dry mixing → wet mixing → SBR addition), and the viscosity is controlled at 2000-4000mPa·s.
Key equipment: vacuum mixing machine, nano sand mill, ultrasonic disperser.
2. Electrode coating - precision determines performance
Coating is the core process of converting slurry into electrode sheets, which directly affects the energy density and cycle life of the battery.
2.1 Classification of coating processes
- Blade coating: suitable for high solid content slurry (positive electrode solid content 60-70%), coating thickness accuracy ±1μm.
- Slit extrusion coating: used for ultra-thin coating (negative electrode surface density 8-12mg/cm²), edge uniformity of ±0.2mm.
2.2 Drying parameter control
- Positive electrode baking: multi-stage temperature zone design (95-120℃), solvent residue ≤2000ppm, to prevent cracking and "orange peel effect".
- Negative electrode baking: low temperature drying (80-105℃), avoid graphite oxidation, moisture control ≤3000ppm.
Technical difficulties: thinning the edge of the electrode sheet (positive electrode thinning 20-30μm, negative electrode 10-15μm), to prevent stress concentration in the ear area and cause lithium precipitation.
3. Electrode Sheet forming
The coated electrode needs to be compacted, slitting, and battery tab welding to form a standardized electrode assembly.
3.1 Rolling process
- Cold pressing and hot pressing: Hot pressing (80-120℃) can increase the compaction density (LFP reaches 2.4-2.6g/cm³) and reduce the rebound rate (positive electrode ≤3μm).
- Elongation control: positive electrode ≤0.2%, negative electrode ≤0.12%, to avoid breakage during winding.
3.2 Slitting and tab welding
- Slitting burr detection: laser secondary element measuring instrument is used, burr height ≤1/2 diaphragm thickness (such as 20μm diaphragm, burr ≤10μm).
- Ultrasonic welding: positive aluminum pole ear welding strength ≥8N/mm², negative nickel pole ear uses linear welding head to prevent overcurrent damage.
Key equipment: high precision roller press, electrode slitting machine, battery tab spot welding machine.
4. Battery cell assembly
The precise lamination design of electrode sheets and diaphragms is the core guarantee of battery cell safety and energy density.
4.1 Winding process
- Tension control: positive electrode tension 0.08-0.15MPa, diaphragm tension difference ≤0.03MPa, to prevent wrinkles and broken belts.
- Alignment accuracy: negative electrode width > positive electrode 1.5mm (such as positive electrode 58mm and negative electrode 59.5mm), diaphragm centering deviation ≤±0.3mm.
4.2 Shelling and liquid injection
- Vacuum drying: 80℃ baking for 4 hours, moisture content ≤500ppm, to avoid electrolyte decomposition.
- Electrolyte injection: nitrogen protection in the glove box (oxygen content ≤10ppm), injection amount error ≤±0.1g, immersion time ≥8 hours.
Technical breakthrough: stacking process replaces winding (such as blade battery), space utilization rate increased by more than 15%.
5. Post-processing and testing: Activating the "life" of the battery
The battery cell needs to undergo complex processing such as formation, capacity division, and aging before it can be transformed into a qualified finished product.
5.1 Formation process
- First charge and discharge: 0.02C small current activation (voltage 3.0-4.2V), SEI film formation temperature is controlled at 25±2℃.
- Exhaust treatment: high temperature pressurization (60℃/0.5MPa) to discharge residual gas and reduce the expansion rate.
5.2 Capacity grading and screening
- Capacity grading: 0.5C charge and discharge cycle, capacity deviation ≤±3%, internal resistance difference ≤5%.
- K value test: voltage drop ≤5mV after standing for 72 hours, screening self-discharge abnormal battery cells.
Intelligent upgrade: AI visual inspection system achieves a detection rate of pole piece defects (black spots, scratches) ≥99.9%.
"Capacity grading: during the manufacturing process of batteries, due to process reasons, the actual capacity of the battery cannot be completely consistent. The process of classifying batteries by capacity through certain charge and discharge tests using battery charge discharge test equipment is called capacity grading."
The main production process of lithium batteries (Cylindrical Cell)
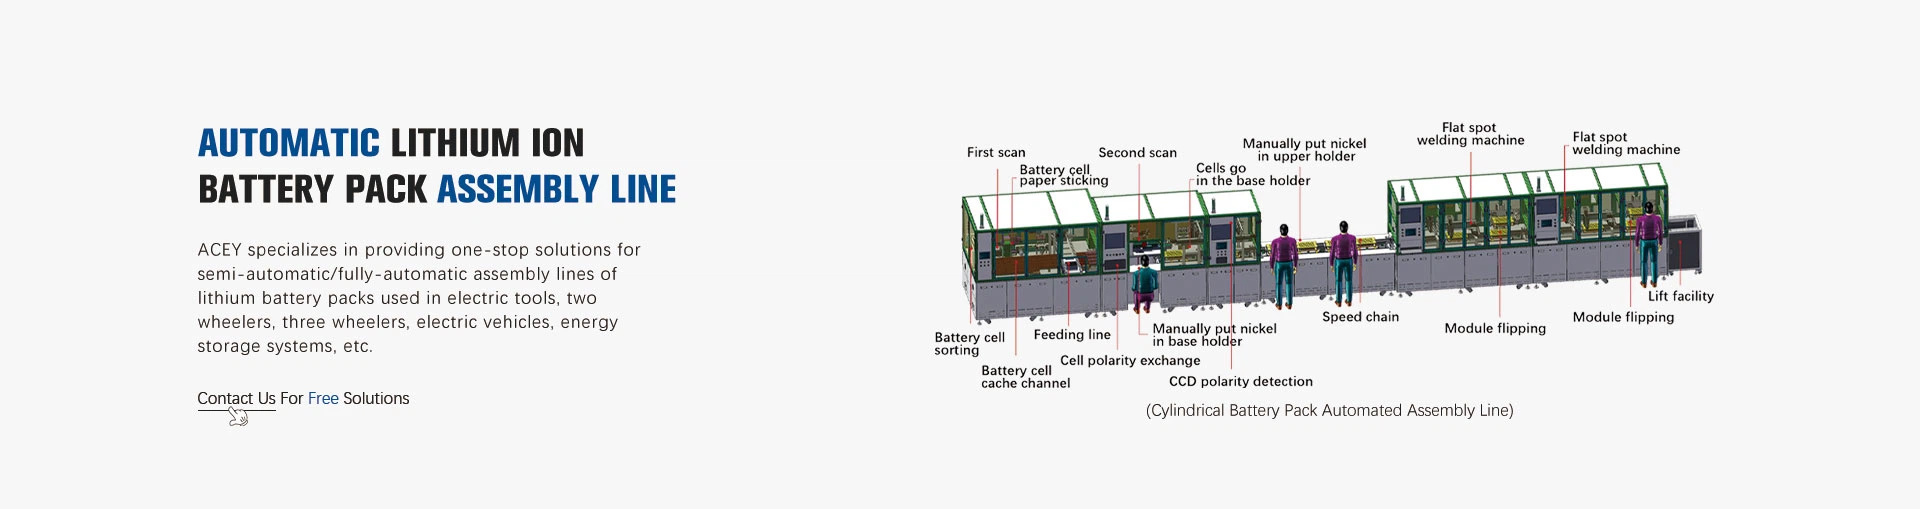
Positive & Negative electrode material homogenization ➯ Electrode coating ➯ Electrode rolling ➯ Electrode slitting ➯ Electrode drying ➯ Electrode winding ➯ Jelly roll insertion into can ➯ Negative electrode welding ➯ Case grooving ➯ Cap Welding ➯ Vacuum drying ➯ Electrolyte injection ➯ Electrolyte Diffusion ➯ Battery Sealing ➯Battery Formation
"Battery Formation: after the assembled battery is given a certain current, the active materials of the positive and negative electrodes of the battery are stimulated, and finally the electrochemical process that makes the battery have discharge capacity is called formation. The battery can only be used as a power source after formation."
6. Environmental protection and recycling
Lithium battery production needs to take into account efficiency and sustainability, and closed-loop management is required from dust recovery to wastewater treatment.
6.1 Dust recovery system
- Positive electrode dust: bag dust removal + activated carbon adsorption, recovery rate ≥ 98%.
- NMP recovery: distillation tower purification, solvent reuse rate ≥ 95%.
6.2 Wastewater treatment
- Fluoride-containing wastewater: chemical precipitation + reverse osmosis treatment, fluoride ion concentration ≤ 10mg/L.
- Graphite sludge: high temperature calcination to prepare recycled graphite, resource utilization rate ≥ 80%.
Three major evolutionary directions of future processe
Solid-state battery process: dry electrode technology eliminates the use of solvents and reduces energy consumption by 40%.
Extreme manufacturing: 4680 large cylindrical battery cell with full-ear design, the production cycle is increased to 300PPM.
Digital twin: Virtual simulation of the entire process from slurry dispersion to formation, reducing trial and error costs by 70%.
From nano-scale material dispersion to intelligent quality control, lithium battery manufacturing is a precise symphony spanning the micro and macro levels.